Filed under frosted glass bottles — start there for the stock moulds, then use the detail below to narrow the spec.
A low-gloss glass bottle is made in one of two ways: a lacquer with matting agents is sprayed on and cured, or glass is taken off the surface by acid, laser or abrasive blast. The sprayed film gives tight colour and gloss control but can burnish, mark and soften in alcohol; the etch is permanent but cannot be colour-matched or repaired. Whichever route is chosen, it only holds up in a dispute if the gloss is written as a number in gloss units, the colour as an instrument reading, and the rub, solvent, adhesion and downstream trials are agreed on a signed sample before the run.
Matte, frosted and etched are not synonyms
Briefs use the three words as if they were one. They are not: "matte" and "frosted" name a look, while "etched" names a method. Ask for an etch when a hazy lacquer was meant and the supplier will price a different article from the one you pictured.
In the glass packaging trade, matte means a low-gloss applied film. Matting agents in the lacquer leave a fine roughness at the top of the cured layer, and that roughness scatters light instead of mirroring it. The glass beneath is untouched. A clear matte keeps the body colour and only removes the shine; a pigmented matte supplies the colour itself, and the glass is reduced to a carrier. Most glossy coloured bottles on a shelf are clear glass under an opaque film, and their matte versions are that film with the gloss taken out.
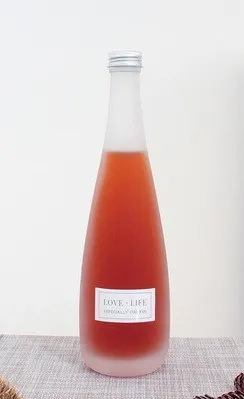
Frosted means hazy and translucent, and it can be reached from either direction. A decorator may spray a transparent matte coat and call it frost, which is fair at arm's length. Or the frost may be real: glass removed by a hydrofluoric-acid-based etch that dissolves the silica network, by a laser that micro-fractures or ablates the surface, or by a hard medium blasted against it. In a photograph the film and the etch are hard to tell apart. In service they have little in common.
| Property | Sprayed film (additive) | Etch, laser or blast (subtractive) |
|---|---|---|
| Where the effect sits | In a layer tens of microns thick on top of the glass | In the glass surface itself |
| Optical character | Scatter at the outer surface; can carry its own colour, or let the body colour tint it to a soft pastel | Scatter inside a shallow layer of glass, so the haze has visible depth and always takes the body colour |
| Touch | Slightly warm, dry, softly grippy; often called soft-touch even when the lacquer is not strictly one | Cooler and harder, like smooth wet stone, because skin still meets glass |
| How it fails | Can be damaged, removed, or attacked by the solvents that attack any coating | Cannot peel or rub off, but cannot be touched up either if it comes out wrong |
The touch row matters more than it looks. A hand reads the surface before an eye reads the label, so a brand that chose matte for the feel should know that a frosted film and an etched body feel different even when a rendered mock-up shows them as identical.
None of these terms is an on/off switch either. Between full gloss and dead flat the trade loosely names eggshell, satin, semi-matte and matte, and the only firm description is a gloss-meter reading at a stated angle. Two suppliers can each deliver "matte" and be twenty gloss units apart, which is obvious once the bottles stand side by side. A finish without a number is not yet a specification.
Process routes for a low-gloss bottle
Eight routes are realistically available. The tables below are meant to produce a shortlist, not a specification; the last column lists what must be answered before committing, and for several routes the honest reply depends on the container geometry, the batch and the product chemistry. Matte is one branch of the wider lacquer family described in our overview of spray coating on glass bottles, where the general adhesion logic is set out. Metallising, plating and vacuum deposition are a separate reflective family with their own wear behaviour and acceptance method, and are not part of this comparison.
Sprayed routes
| Route | How it is made | Look and feel | Wear | Print, label and line effects | Typical use | Confirm before committing |
|---|---|---|---|---|---|---|
| Clear matte lacquer on bare or coloured glass | Transparent lacquer with matting agents, sprayed and cured; the glass still supplies the colour | Dry, silky, lightly grippy, no specular highlight; amber becomes a muted amber | Rubbing polishes the texture into a glossier patch; hand oil darkens it locally; alcohol resistance rests entirely on the top-coat chemistry | Gives screen ink tooth; pressure-sensitive labels wet out slowly and a clear label may show a silvered halo; more friction on rails and screws than gloss glass | Spirits, olive oil, kombucha, premium water, wherever the glass colour should keep doing the colour work | Target gloss and tolerance band, where on the container it is measured, the rub-test solvent, the wash regime |
| Coloured matte lacquer, single coat | Pigmented matte lacquer in one pass, so the body can be flint whatever the colour | Flat, even colour from every angle; a light tone over flint may grin or thin out at sharp radii | Burnishes and oil-marks like any matte film; the critical defect is a thin edge or coverage gap reading as a lighter patch, with no spot repair | Very good print key; a light colour over dark glass may need a second pass, adding cost and steps to qualify | Mass and mid-market lines repeating a brand colour on flint with a softer look | Whether one coat fully hides the glass, whether a base coat is needed, how colour is read on a curve |
| Two-coat system, base coat plus matte top coat | A primer or base coat sets colour and hides the glass; an unpigmented matte top coat sets gloss; each can be tuned alone | The most controlled sprayed matte: tight colour match, gloss adjusted without shifting tone | Usually the toughest sprayed matte, since a cross-linked top coat can be formulated for abrasion and solvents; mask edges stay the weak point | Print and foil sit on the top coat and qualify separately from colour; the extra pass multiplies handling, mask edges and contact marks | Colour-matched premium lines, gift and limited editions, tolerances too tight for a single pigmented coat | Total film thickness, which layer carries colour, cure schedule per layer, how the stack performs in the rub test |
| Frosted lacquer, a hazy clear coat sold as frost | Transparent matte or hazy coat imitating etched glass; the glass is untouched | Convincing at arm's length and in photos, with less depth than a true etch; tinted by the glass below | Wears as a coating: burnish, scratch, solvent attack; an aggressive cleaning process can strip it completely | Behaves as any matte film; hidden entirely under a full-body sleeve, so check what the consumer will see | The frosted look on a coating budget, or shapes where a real etch is not available | How the frost is achieved, that a film rather than an etch is being accepted, how haze is measured lot to lot |
Routes that remove glass
| Route | How it is made | Look and feel | Wear | Print, label and line effects | Typical use | Confirm before committing |
|---|---|---|---|---|---|---|
| Full-body acid etch | Acid-based chemistry applied, usually through a resist, then rinsed and neutralised | Permanent milky satin with real depth; an amber bottle becomes a pale amber haze | The most abrasion-tolerant low-gloss route; a deep scratch is permanent, and the pores can hold hard-water deposits and residue | Surface chemistry changes along with roughness, so labels must be trialled on the etch itself; harder and cooler in the hand | Premium spirits and fragrance, boutique oil and vinegar, finishes that must outlast the pack | Etch depth and haze level, whether the mould seam shows afterwards, wash behaviour, mechanical performance after material removal |
| Masked acid etch or etched pattern | The same chemistry through a patterned resist, giving frosted logos, bands, florals or windows on clear glass | Sharp satin-against-clear contrast with no step or ridge, because no film edge exists | As durable as the etch; the boundary is a permanent feature, not an edge that can lift | Either zone takes print or foil; the resist artwork is tooling to make and store, and any pattern change is a new setup | Logo-led, heritage and craft designs built on a frosted graphic against gloss | Who holds the resist artwork, what run a pattern requires, how fine a line holds without undercutting |
| Laser frost, no acid | A focused, programmed beam alters the surface point by point; no resist and no blast medium | Fine, uniform frost with accurate placement; small text, serial marks and fine graphics an acid resist would struggle with | Permanent; depending on parameters, somewhat more prone to handling marks than a chemical etch | Best for small marks and data, not whole bodies; a separate step with its own cycle time; can mark beside a label window without masking | Traceability marks, batch codes, small logos on a glossy or matte body | Cycle time per container, smallest reliable feature, rub and wash behaviour of the marked area |
| Sandblasted frost, full or masked | Hard abrasive projected at the glass, across the body or through a protective mask | Coarser and more open than acid etch, sometimes plainly grainy; varies with medium, pressure and nozzle distance | Permanent, but the most mechanically aggressive subtractive route, so the container's surface condition belongs in the decision | Rough surface can abrade labels and trap residue; mask edge is sharper than a coating edge but still visible; hard to hold uniform on complex shapes | Decorative pieces, rustic and craft positioning where the coarse texture is the intent | Uniformity over the whole body, effect on surface condition, appearance of the masked boundary |
Read together, the sprayed routes win on control and colour freedom, and the subtractive ones win on permanence. Two questions that are not about appearance usually settle it. If the finish must not depend on a film that can fail, choose an etch. If the colour must sit tightly on a brand standard, choose a two-coat spray. Buyers who need both often end up with a matte body plus an etched or blasted accent, or an etched body carrying print, and should expect more interfaces to qualify than either route has alone.
What to fix in the finish brief
One decision comes before any of this: whether the colour lives in the glass melt or in a sprayed layer. That choice has its own economics and inventory effects and determines which finishes are available at all, so settle it first using our comparison of raw material colouring and surface spraying.
After that, a matte project has seven adjustable dimensions. Taking them in order avoids the familiar surprise where a colour and a coverage pattern turn out to be incompatible at the gloss level requested.
- Effect family. Applied matte coat, frost coat sold as matte clear, acid etch, laser frost or blasted frost.
- Base glass colour. The body the effect sits on or is worked into.
- Coverage pattern. Full-body wrap, body with a clear or glossy neck, horizontal band, vertical stripe, shoulder-only or base-only, a clear label window, a logo cut-out showing gloss against matte, or a graded fade from matte to gloss.
- Gloss level. Anywhere from soft eggshell to deep flat matte.
- Film tone. Clear over the glass colour or pigmented; solid, two-tone, or laid over an earlier base coat.
- Other decoration. Glossy screen print, a hot-stamped logo, a clear gloss drop, or a partial sleeve on the matte ground.
- Mask geometry. The exact outline of every zone that must stay free of film or etch.
Coverage is where most of the design freedom sits, and most of the process cost. Each pattern in that list is a mask. A mask means another operation and, more to the point, another edge, and edges are where coatings lift and etches undercut.
Zones that always stay bare
Two areas are excluded for function, not style. One is the inside of the container. The other is the neck finish: threads, crimp ledge and every sealing face. Lacquer on a thread alters the dimension the closure was built to fit, gets abraded by the closure in use, and can shed particles towards the product. Lacquer beneath a crimped ferrule tends to leak once the temperature shifts. An etch is worse, because reaching a sealing face means the seal surface itself has been changed.
Draw both as no-coat or no-etch zones on the artwork and have them confirmed in writing. Do not leave them to the decorator's discretion. Other feasibility limits are mostly a matter of geometry, covered further down.
Dark and light mattes behave as separate projects
Keep the route, the supplier and the nominal gloss constant, change only the tone, and the project still changes, because the film has a different job and the eye looks for different faults.
| Aspect | Light matte (white, cream, pale pastel) | Dark matte (black, deep tones) |
|---|---|---|
| Hiding power | Needs high pigment loading and often a base coat to stop the glass showing through | Far more hiding per micron; fewer coats, more tolerant of coverage variation |
| Where it fails first | Wherever spray runs thin: tight radii, the shoulder-to-neck transition, mask edges | Gloss shifts, which read as a change in depth |
| What it reveals | Anything dark: plant dust, a speck in the film, fingerprints, oil smudges, scuffs that have picked up dirt | Anything light: lint, dust fibres, burnished sheen, lifted scratches, the bloom of an over-handled film |
| Uniformity risk | Small changes in film thickness or pigment dispersion show as patchiness, since little chroma masks them | Thickness variation is mostly hidden; a few gloss units of drift is not |
| Acceptance method | A tight numerical colour tolerance | A tight gloss band plus a visual check under two light sources |
This is why matte black is the easiest matte to specify and matte off-white among the hardest, a gap that appears in both the count of process passes and the reject rate. A plant accustomed to glossy bottles will also find that a light matte exposes contamination it has always been able to hide, so an inspection regime tuned for one tone cannot simply be carried over to the other.
The glass body is a third variable. Hiding amber under a dark matte can take more film than hiding flint, and light mattes are nearly always specified on flint so no body colour interferes. Decide body and finish together, using the guide to standard and specialty glass colours to pick the substrate. For a deep matte black the body barely affects the colour but directly affects the number of coats; a quote for matte black that never asks about the body may be one pass short. If the bottle itself is all you need, the catalogue page for matte black glass bottles lists capacities, shape families and stocked options.
How the bottle shape limits the finish
Gloss describes form with light. A highlight running along a shoulder, a bright band on a facet, a dark line at a radius: these tell the eye whether a bottle is round, faceted or tapered. Matte deletes nearly all of that, leaving silhouette, colour and shadow. A bold, simple form survives on those. A gentle taper with a soft shoulder may collapse into a plain cylinder, and the cure is either firmer geometry or a deliberate highlight brought back through a gloss or metallised accent.
- Moulded detail. Flutes, facets and embossing still show through a matte film, but less crisply; fine detail that looked like jewellery in gloss can flatten into mere texture.
- Mould seams. Under a matte coating the scatter largely hides the seam, which helps. Under an etch the opposite can happen: the chemistry may act at a different rate where the surface condition changes, turning an unnoticed seam into a visible line. Inspect it on the real container.
- Weight and wall. With the light flattened, the eye judges mass and proportion. A light matte on thin-walled glass tends to look inexpensive, and a heavier base or thicker wall often lifts perceived quality more than any finish change. Raise this at the mould stage, when it costs far less than a finish problem found at sampling.
- Radii and neck transition. Spray thins at sharp transitions and tight concave radii, so a light matte can look washed out exactly where shoulder meets neck. Generous radii and two-coat systems both help. Ask the decorator to name the thinnest point on the container before the design is frozen.
The thread and seal exclusions hold on every shape, since they are dimensional and sealing requirements. Finish that strays into a thread is a functional fault, not a cosmetic one.
Effects on labelling, printing, sleeving, washing and capping
The finish becomes the surface that every later operation has to work against. Its effects are regular enough to plan around.
Pressure-sensitive labels
Adhesive has to flow into a matte film's texture before it reaches full contact, and that flow is slow. The signs are a silvered or hazy halo behind a clear label, small edge bubbles, and a label that passes at the applicator and lifts at a corner a week later. Clear labels are the worst case because the halo looks like a fault. Trial the production label stock on the production surface and allow a dwell period before judging. Where the design permits, leave a glossy window as the label panel so the bond is the same as on a gloss bottle, accepting that the window is a mask with its own step and edge.
Etched and blasted glass is a different case again. Frosted glass is more hydrophilic than lacquer, which can help wetting, while its roughness cuts the effective contact area; the net result can only be found by trial. The frost also shows through a clear label. Wet-strength and wash-off labels need particular care here, since a label designed to release in a wash bath may not release from a textured surface in the expected time.
Screen print and hot stamping
Matte is usually the easier substrate. The texture that scatters light also keys the ink, so adhesion is often better than on a fully glossy film, and gloss print on a matte ground is an established device because the contrast looks intended. Two risks remain. An ink or its thinner can partly soften the top coat and leave a bloom or dull patch that only appears after cure, so qualify that ink with that top coat. And thin foil can telegraph the texture below it; a heavier foil or a print primer may be required for a crisp mark.
Shrink sleeves
Start by asking whether any finish stays visible. A full-body sleeve hides the body entirely, so matte under it is money spent on a surface nobody sees. If the matte is part of the design, use a partial sleeve, a neck band or a windowed sleeve. Where the sleeve does sit on matte, the extra friction can upset a high-speed sleever: containers that grip instead of slide may mis-feed or mis-orient, and the sleeve can wrinkle where it catches. Only a line trial answers this.
Washing
Sprayed matte and a hot alkaline returnable-bottle washer do not mix. Caustic and heat are hostile to the film, which may dull, whiten or lift. Etched glass copes better with the hot wash, yet its pores hold residue and hard-water deposits, so bottles can emerge chalky instead of cleanly frosted. For any refill or return scheme, put the wash regime into the finish specification before picking the route.
Capping
Coating or etch changes the friction between closure and glass. Re-qualify application and removal torque bands on the decorated container instead of inheriting them from the plain-bottle programme, and keep the sealing surface and ferrule seat as clean glass.
How a matte surface wears in use
A specification written for gloss glass will miss what happens to matte, because the wear looks different. Four mechanisms account for nearly all of it.
Burnishing. A finger, a cloth, a guide rail or a neighbouring bottle polishes the roughness that creates the scatter. The rubbed area turns glossier: a shine in flat black, or a lighter, smoother patch on a pale tone. No film has been lost, so a test that looks only for film removal will pass it. The failure is properly defined as a rise in gloss reading after a set rub, and an abrasion test on matte should report gloss change, not just weight loss or a visual pass.
Hand oils and sweat. Sebum and hand cream fill the texture; a filled texture scatters less, so the touched area darkens and glistens. Pale mattes show dark fingerprints, dark mattes an oily sheen. The remedy in both cases is a mild cleaning agent and a soft cloth, never a solvent wipe. Channel matters: a tester bottle in a department store or a pack kept in a bathroom collects marks that the same pack shipped sealed from an online order never will.
Alcohol and solvents. This is what most often divides an acceptable matte from a failed one. Ethanol-based contents reach the outside of the pack on the consumer's hands, and hand sanitiser is now a routine exposure. A matte film has more surface area than a gloss film, so there is more for a solvent to attack, and a formulation that survives on a glossy bottle may fail on its matte twin. Oils and water-based cosmetics are forgiving; fragrance and sanitiser packs are the hard end. The deciding test is a double rub with a solvent chosen by reasoning from the product, not by habit.
Scratching. Matte is often a little softer than a fully cross-linked gloss and scratches more easily, but the scratch tends to show less: on gloss it flashes, on matte it may only strip the matting and leave a faint glossy line. Etched glass tolerates scratching best among the low-gloss routes, though a deep scratch in etched or blasted glass is permanent and will not polish out.
For all four, measure against a defined rub under a defined light source. Sodium or fluorescent factory lighting conceals precisely the sheen and oil marks a consumer will see in daylight.
Why brands accept the loss of transparency
The case for matte is optical. A glossy bottle throws a specular highlight that shifts with the lamp, the viewer and the shelf, so it is bright in one spot, dark in another, awkward to photograph without glare and hard to light evenly across a range. A matte bottle spreads the same light, reads consistently from any angle, photographs without a hot spot and keeps its look under mixed retail lighting. For a brand that has to print a catalogue, stock a shelf and shoot a campaign with one bottle, that predictability is the benefit.
There are two further reasons. Matte is pleasant to hold and grips slightly in a wet hand, signalling care much as uncoated paper stock does. And among glossy neighbours it is the one surface not reflecting the lighting rig, a difference visible from further away than the label can be read. Skincare and serums, premium spirits, boutique olive oil and vinegar, kombucha and cold brew, candles and home fragrance, supplements and premium water use it most. In each, the formulation or origin story is what is sold, not the sight of the liquid.
What is given up is recognition: the fill level, clarity and colour of the contents can no longer be seen. That costs little for a uniform product whose label carries the identity. It costs more in four situations:
- naturally variable products such as unfiltered juice, cold-pressed oil or small-batch spirit, where the look of the contents signals quality;
- refill or returnable schemes, where the user needs to see how much is left;
- categories in which shoppers judge freshness by colour;
- small packs whose label area is too limited for print to carry the whole identity.
Design, not process, pays this cost back. A clear window can be masked out as a horizontal band, a vertical stripe, a shoulder or a base. A glossy label panel fixes visibility and label adhesion with a single mask and looks deliberate. A glossy or metallised accent such as a logo, a rim or a gloss drop gives the eye a focal point; on dark matte it is what makes the pack look considered instead of simply dark, while on light matte it reads as a detail. Identification can move wholly to silhouette and typography, which explains why so many matte lines pair a distinctive form with a large, quiet label. On a small pack, a clear neck band or a moulded level mark does the job. Every window or panel is a mask and an edge, so it must be drawn and qualified like any other boundary.
From drawing to production sample
Costly errors in matte work usually come from a skipped step, not a wrong process. The sequence we coordinate between a buyer and the decorating plant has ten stages.
- Physical effect brief. A render cannot be measured and matte shifts sharply with lighting. Supply a named reference object that can be held, or a measured colour and gloss target, plus the coverage and the clear zones.
- Route selection from the comparison tables above.
- Substrate. Clear or pigmented film; whether a light matte needs an opaque base coat so the glass cannot grin through; flint, amber or another body.
- Coverage drawing with mask zones, label window, and neck and seal exclusions marked as no-coat or no-etch areas, not described in words.
- Samples in two stages. An effect panel establishes colour, gloss and texture quickly and at low cost. A decorated sample on the real geometry then shows how spray covers a shoulder radius, how film crosses a mould seam and how an etch wets the neck transition. A supplier offering only a panel has not tested the design on what will ship.
- Downstream trial. The production label stock applied, the production ink printed and cured, the sleeve run, and a sample put through the intended wash. This is the stage most often dropped and the source of most complaints after launch, yet on a handful of samples it costs little.
- Golden sample. A single unit, signed and dated, held by both sides under matching storage conditions and taken after the final effect step. One pulled from an intermediate stage looks authoritative and is wrong.
- Acceptance protocol. Which measurements, on which areas, how often, to what tolerance, with critical, major and minor defects defined in the language of the AQL and ISO 2859-1 families.
- Process record. Coat weight or film thickness, gloss reading, colour reading and cure conditions behind the golden sample. Without it, a reorder eighteen months on is an approximation.
- Handling and packing specification. A bottle that leaves the plant perfect can still be burnished inside a shipper cavity.
Tests to run before signing off the sample
A matte sample can be approved by eye in thirty seconds and fail in the field three months later. Each check below can be run on a few containers ahead of any production order.
| Check | Method | What to pin down |
|---|---|---|
| Colour | Instrument reading on an agreed flat area of the finished container, never on a separately sprayed panel; visual confirmation under a daylight-equivalent source such as D65 and again under a warm retail source | Illuminant and observer agreed before the first sample; tolerance as a numerical colour difference, not an adjective |
| Gloss | Gloss meter at a defined angle, conventionally 60 degrees for a mid-range surface and 85 degrees for a low-gloss matte, reported in gloss units | Target and permitted band as numbers; measurement points such as shoulder, body and base marked on a drawing |
| Abrasion and burnishing | Defined rub or rotary abrasion in the tradition of the ASTM D4060 family | Wheel type, load and cycle count; result reported as change in gloss and appearance |
| Solvent and alcohol | Double rub with a nominated solvent: an ethanol-and-water blend approximating fragrance for a fragrance pack, isopropanol as a general check, or a MEK rub in the ASTM D4752 tradition where the purchase specification requires it | Judged for gloss change, softening and breakthrough on the finished stack, since the top coat decides the result |
| Adhesion | Cross-cut tape test in the ISO 2409 or ASTM D3359 tradition on the finished container, at the tightest radius in the design | Tape type recorded, because a different tape changes the outcome |
Some notes on reading these. Matte is easier to measure for gloss than a metallic finish, being diffuse instead of gonioapparent, but the reading still responds to spot position and curvature. In abrasion, the figure that counts is the rise in gloss: a test that looks only for breakthrough will pass a surface that has already gone shiny. In adhesion, classify honestly, because the texture makes a small departure from the reference chart easy to explain away. If the pack will live in a bathroom or travel in a bag, add a wet rub or artificial-sweat check on the same sample. A colour that matches in daylight can also drift under shop lighting, hence the second viewing.
Two further groups complete the sign-off. The downstream checks repeat the trial stage on the approved finish: label applied and left before judging halo and edge lift, ink printed and cured, sleeve run and examined for wrinkles, a sample washed as the pack will be, and every mask boundary inspected for bleed, a step in gloss and feathering. The environmental checks cover humidity, immersion and a thermal cycle when the pack will meet extremes or ship by sea. Record the results alongside the golden-sample data so a reorder is reproduced, not renegotiated.
What drives cost and the minimum order
We do not publish a unit price, tooling cost or minimum quantity for matte work, because none can be stated until the route, the treated area and the batch are fixed. Each is quoted per project. What moves the quote is the number of operations and the risk attached to each:
- Route. Spray and etch have different cost structures, not different prices for one job. Spraying is a decorating operation in a controlled plant. Acid etching adds a resist or mask to make, acid handling, rinse and neutralisation, and a waste stream to manage.
- Passes. A single pigmented matte, a clear matte over existing colour and a primer-plus-top-coat system are three different amounts of work. A light opaque matte generally needs one more pass than a dark one.
- Mask complexity. This surprises buyers most. A clear window plus a logo cut-out plus a banded base is a different job from a full wrap in the same colour. The count of boundaries matters more than the area covered, since labour and risk sit at the boundaries.
- Tightness of target. A narrow gloss band and tight colour tolerance demand more process control and inspection. They are also the two items most likely to be disputed after delivery if never written as numbers.
- Later decoration. Print, foil and sleeve are further operations on a surface that must accept them, and an incompatibility found late is expensive.
- Reject rate. A thin patch, a speck or a burnished edge cannot be polished or touched in without leaving a mark, so cosmetic rejects become scrap instead of rework. That rate is inside the quote whether itemised or not.
- Order size, because setup is spread over the run.
The minimum is set by process setup, not by the glass. A one-colour full-body spray and a two-colour masked etch sit far apart: the etch needs resist artwork, the coating supplier may have a minimum material batch, and a tight colour match may call for a dedicated sample lot first. Since the minimum shifts with route, tone, mask artwork, covered area and batch, any published figure would mislead, and it is confirmed on inquiry once route and artwork are settled. The cost of the undecorated container is a separate matter, covered in the glass bottle price breakdown.
Common complaints and who carries them
Complaints about matte bottles fall into five recognisable types, and most can be assigned to a cause before the goods even arrive.
- Sample-to-delivery difference: gloss above or below the approved unit, colour drift, a spray band or visible edge, a contamination speck, a coverage gap at a shoulder or radius.
- Wear in the consumer's hand: sheen on the grip area, oil marks that will not clean off, a scuff ring where bottles touched in the shipper, matte turned glossy after washing.
- Interface failure after filling: label edge lift, a silvered halo behind a clear label, sleeve wrinkles, ink bloom at the top coat, a torque band that no longer seals properly.
- Structural failure at a mask boundary, where coating lifts from the edge.
- Product-related failure, where the surface passed a dry rub and failed an alcohol rub because the contents are ethanol-based.
Four instruments, agreed before production, draw the line of responsibility: the signed golden sample held by both parties; the written acceptance protocol; a defect classification in AQL and ISO 2859-1 vocabulary; and an agreed inspection point. In practice that point has to be a pre-shipment inspection at the plant, to a defined sample size under stated lighting. Judging matte in destination lighting after a sea voyage means judging two changes at once.
| Sits with the supplier (present before shipment) | Sits with the buyer or downstream parties (introduced afterwards) |
|---|---|
| Coverage gaps, spray bands, mask bleed | Contact marks from guide rails, star wheels, feed screws and transfer plates on the filling line |
| Gloss outside the agreed band; colour outside tolerance | A shipper cavity that lets units grind against each other |
| Contamination in the film; failure of the agreed rub test | Product chemistry that was never disclosed and so never tested against the finish |
| Adhesion failure at a radius | A wash regime the finish was not qualified for |
| An etch that undercut the resist or gave inconsistent haze | An acceptance protocol left unwritten, so no standard exists to measure against |
Some wear is shared. A heavily handled channel will mark a matte surface, and a supplier who knew the channel and still proposed the finish carries part of that risk. Modest habits head off most disputes: keep a signed golden sample per colour and gloss level, keep a sample from every lot, photograph the packed configuration as shipped, inspect to the agreed plan before dispatch, and decide beforehand how a rejected unit is treated. That last point weighs more on matte than elsewhere. Coated or etched glass cannot be polished or spotted in, so a reject is normally scrap, and agreeing so early avoids a late quarrel over whether a unit was repairable.
Frequently asked questions
How does a matte bottle differ from a frosted one?
Both words describe a look, but the usual production differs. Matte normally means a sprayed low-gloss film that scatters light at the outer surface and may carry its own colour. Frosted can be the same thing done with a hazy clear coat, or it can be glass altered by etching, laser or blasting, where light scatters within a shallow layer and the haze takes on the body colour. Depth is the visual tell. Damage is the practical one: films fail, etches do not.
Does an etched surface outlast a matte coating?
Yes. An etch belongs to the glass and has nothing to peel or lift, while a cured film burnishes, scratches, and can soften or dull under alcohol or hot alkaline washing. Durability is seldom the only criterion, though. Coating reaches colours and gloss levels an etch cannot, goes onto almost any geometry, and is generally the less costly route. Most buyers coat when colour flexibility leads and etch when the finish has to outlive the pack.
Will labels and screen print hold on matte glass?
Both are routine, provided each is qualified on the matte surface in question and not carried over from a gloss programme. Ink keys well into the texture. Pressure-sensitive labels are the cautious case, since slow wetting can leave a halo behind clear stock or edge lift days later; a dwell-time trial and, where possible, a glossy label panel are the standard answers.
Will a bottle washer strip the finish?
A hot alkaline returnable-bottle washer can dull, whiten or lift a sprayed matte. Etched glass withstands the wash better but may come out chalky from deposits lodged in its pores. Choose the finish for the cleaning process by writing the wash regime into the specification first, instead of finding the mismatch in a trial wash after the containers exist.
Why do fingerprints and shiny patches appear?
They share one cause: anything that fills or flattens the micro-roughness changes how that spot scatters light. Oil fills it, making the area darker and slightly greasy, most noticeably on pale tones. Rubbing flattens it, making the area glossier, most noticeably on dark ones. Neither counts as a defect in the usual sense. Gentle cleaning and a thoughtful choice of tone manage both, and a pack that will be handled often should be specified with them in mind.
Can part of the bottle remain clear?
Yes. A masked window, a vertical stripe, or a bare shoulder or base lets the consumer see fill level and contents while the body stays matte, and the opening can be left as clear glass or finished as a glossy panel. The price is one more mask, one more process step and at least one more edge where coating can lift, so it goes on the artwork and through qualification instead of being agreed in conversation.
What should an inquiry for a matte finish include?
Start with three items: the intended effect, the container and the annual quantity. Give the effect as a physical reference or measured target and say whether a coating or a true etch is meant. Describe the container with its body colour, the coverage wanted and the zones to keep clear, neck finish and sealing surfaces included. State quantity per year, not per order, since it decides whether dedicated mask or resist artwork is economic. Then add the product chemistry, the sales channel, the wash regime for refillable packs and the label or sleeve to be used. With that, we can propose a route and its validation items in one round.